Hey everyone, if you’re in aerospace machining, you know Linear Milling Machines aren’t just a “nice-to-have”—they’re the backbone of getting those super tight, zero-defect parts right. I’ve been supplying these bad boys for over a decade, and let me tell you, I’ve seen shops skip key requirements and end up wasting weeks (or months) fixing botched parts. Today, I’m breaking down exactly what you need to lock in before you even fire up a Linear Milling Machine for aerospace work. No corporate jargon, just real talk from someone who’s on the floor with machinists and engineers every week. Linear Milling Machine
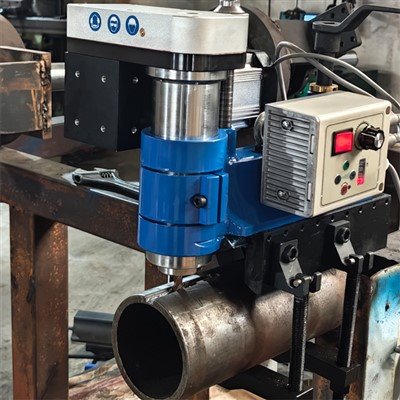
First off, let’s get one thing straight: aerospace parts are not your average auto components. We’re talking turbine blades, wing spars, landing gear brackets—parts that operate in 1,500°F heat, under 10+ tons of pressure, and have tolerances so tight you could fit a human hair 10 times between the part’s edge and its spec. A Linear Milling Machine’s core design is what makes it ideal here (no rack-and-pinion slack, thanks to linear guides and direct-drive motors), but that only works if you nail three foundational requirements first: structural rigidity, precision calibration, and thermal stability. Let’s dive into each, because cutting corners here is a one-way ticket to scrap heaven.
Structural rigidity is non-negotiable, but not just any rigidity—aerospace-specific rigidity. Most general-purpose mills use cast iron frames, but aerospace Linear Milling Machines need a frame that can handle both heavy cuts (think 300+ ipm feed rates on titanium) and tiny, delicate cuts (like trimming a turbine blade’s 0.2mm wall without deflecting). I can’t tell you how many times a shop brought in a used Linear Mill for aerospace work, only to find the base was warped from years of bad setup on a concrete floor that couldn’t support the 12,000-pound machine. Here’s the real tip: when vetting a machine, check if its frame uses ribbing that’s spaced every 6 inches (not 12 like generic mills) and has a sealed, vibration-dampening core. Also, the linear guides—they need to be cross-rolled, not ball-type. Ball guides are cheaper, but they have tiny gaps that cause deflection when you’re milling Inconel. Cross-rolled guides? No gaps, even under high load, so your cuts stay true. I had a client last month who switched from a ball-guide Linear Mill to our cross-rolled model, and their turbine blade scrap rate dropped 18% in a month. That’s not a sales pitch—that’s real numbers from a shop that was struggling with vibration errors.
Next up, precision calibration—and I mean ongoing calibration, not just the factory test run. Aerospace specs are usually within ±0.0002 inches for critical features, and a Linear Mill’s accuracy degrades if you skip regular checks. Let’s talk about how this works: when the machine is assembled, it uses a laser interferometer to check linear positioning, but that’s just a baseline. Once you move it to your shop, you need a ballbar test every 3 months, and a rotary axis calibration (for 5-axis mills) every month. Here’s a mistake I see all the time: shops use a cheap dial indicator instead of a laser to check X/Y/Z axis accuracy. Dial indicators can only check one point at a time, so you might miss a slope in the axis that’s causing a 0.0005-inch error 10 inches into the cut. That error might seem small, but for a wing spar, that’s enough to make it fail a fatigue test. Also, don’t sleep on backlash compensation—Linear Mills have direct drives, but if the servo motors aren’t calibrated to reverse smoothly, you get a small gap between moves that ruins surface finish. I always tell my clients to set up a calibration schedule that ties into their production downtime, not just when the machine is acting up. Prevention is way cheaper than scrapping a $10,000 part because of a missed calibration.
Thermal stability is the third big one, and it’s the most overlooked. Aerospace materials like titanium and Inconel generate a lot of heat when you mill them, and if your Linear Mill can’t handle that heat, the machine itself will expand, throwing off your cuts. Let’s do the math: a steel linear guide expands about 0.000006 inches per inch for every 1°F rise. If your guide is 40 inches long and the shop temp goes up 10°F while you’re cutting, that’s 0.00024 inches of expansion—right at your tolerance limit. No wonder so many shops have inconsistent parts. So what do you need in a Linear Mill for aerospace? First, a temperature control system for the spindle and linear guides. Not a fancy lab HVAC system (though that helps), but machine-internal cooling: oil jets for the guides, and a spindle chiller that keeps the spindle within ±0.1°F of a set temp. Our Linear Mills come with standard spindle chillers, but I always add the guide cooling as an upgrade for aerospace clients—it’s saved so many shops from last-minute part reworks. Also, make sure the machine’s enclosure is sealed to prevent drafts from doors opening or AC vents blowing directly on the work area. One of my first aerospace clients tried cutting corners here, keeping the door open to load parts, and their blade tips were coming out with 0.0003-inch variations from draft-induced guide expansion. Fixing the enclosure cut their rework rate by 12%—simple, but game-changing.
Now that we’ve covered the machine’s base requirements, let’s talk about operational requirements that are just as important. Even the best Linear Mill is useless if your operator doesn’t know how to use it for aerospace work. First, operator training specific to Linear Milling for aerospace, not just general CNC. A lot of machinists learn on 3-axis mills, but Linear 5-axis mills have feed rates that are 2-3x faster, so you can’t use the same cutting parameters. For example, when milling a titanium landing gear bracket, you can’t use the same feed rate as an aluminum auto part—you need a toolpath that’s optimized for linear motion, not circular interpolation. I offer free on-site training for all my aerospace clients, because I’ve seen shops hire a machinist who’s great at general CNC, and they burn out 3 end mills on a single Inconel part because they didn’t know how to adjust the feed rate for linear guides. Also, aerospace requires traceability—every cut, every tool, every calibration check has to be logged. Your Linear Mill’s CNC system needs to have a built-in data logging feature that syncs with your quality control software. No more handwritten logs that get lost—automated logging ensures that if a part fails, you can trace it back to a specific machine run, calibration date, and tool. That’s non-negotiable for FAA compliance, by the way. I can’t tell you how many shops fail an audit because they skipped data logging for their mill.
Another operational requirement: tooling specifically for Linear Milling and aerospace materials. You can’t use a generic end mill from the local hardware store. Linear Mills run at higher spindle speeds (up to 20,000 RPM for small turbine blades), so your tools need to have a high-performance coating like TiAlN or diamond-like carbon (DLC). Also, tool holders—they need to be HSK-A63 or CAT 5E, not the cheap ER collets that slip at high speeds. I had a client who used ER collets for their Linear Mill, and they had a tool slip mid-cut, ruining a $15,000 titanium bracket. Switching to HSK holders fixed that. Also, tool length compensation—your Linear Mill’s CNC needs to automatically adjust for tool wear, because even a 0.001-inch tool wear on a 10-inch cut can throw off your tolerance. Most modern Linear Mills have this feature, but make sure it’s enabled and calibrated every time you load a new tool.
Wait, let’s not forget about part fixturing. Aerospace parts are often complex, with thin walls and hard materials, so your fixturing can’t just clamp the part anywhere— it needs to hold it without deflecting. Linear Mills have a high movement accuracy, but if your fixturing is warped, the part will move during the cut. I recommend using modular, precision-ground fixturing that’s aligned to the machine’s coordinate system with a laser level. No more manual alignment with a dial indicator— that’s error-prone. One shop I worked with used custom welded fixturing that was off by 0.0008 inches, so their wing spars were failing the alignment test. Swapping to modular fixturing aligned with a laser fixed that in 2 days, no more scrap.
Now, let’s talk about common myths I hear all the time. Myth #1: “Linear Milling Machines are only for large parts.” Nope, we have clients using them for tiny satellite components (1mm precision) and large wing spars (20 feet long). It just depends on the model—smaller linear guides for micro parts, larger ones for big parts. Myth #2: “Any Linear Mill works for aerospace.” Wrong—you need the rigidity, calibration, thermal stability, and operational stuff we talked about. A used Linear Mill from a sign shop isn’t going to cut it (pun intended) for FAA-compliant parts. Myth #3: “You don’t need to calibrate every month.” Wrong—temperature changes, wear on linear guides, and even floor settling will throw off accuracy over time.
So, if you’re in the market for a Linear Milling Machine for aerospace part machining, here’s your quick checklist:
- Structural rigidity: Cross-rolled guides, spaced ribbing, vibration-dampening frame, sized for your max part load.
- Precision calibration: Laser-interferometer-tested at factory, ballbar/laser calibration scheduled monthly, backlash compensation enabled.
- Thermal stability: Machine-internal spindle and guide cooling, sealed enclosure, temp-controlled shop (or local enclosure for drafts).
- Operational prep: Operator trained in Linear Milling/aerospace specs, CNC with automated data logging, HSK/TiAlN tooling, precision modular fixturing.
I’ve been in this game long enough to know that cutting corners on any of these steps will cost you way more in scrap, rework, and audit failures than investing in the right machine and setup upfront. For the shops that follow this checklist, they’re cranking out compliant parts, hitting deadlines, and making money—no headaches, no surprises.
If you’re ready to upgrade your Linear Milling Machine or just want to chat about your specific aerospace machining needs, hit me up for a procurement consultation. No sales pitches, just real talk about what will work for your shop. Let’s get your parts right, together.
Facing Head References
- Aerospace Industries Association. (2022). Precision Machining Requirements for Commercial and Defense Aerospace Parts.
- DMG MORI. (2023). Linear Milling Technology for High-Precision Metal Cutting.
- ISO 9001:2015. (2015). Quality Management Systems Requirements for Aerospace Manufacturing.
- Sandvik Coromant. (2021). Tooling Solutions for Linear Milling of Titanium and Inconel Alloys.
- American Machinist. (2022). Thermal Stability in CNC Machine Tools: Key to Aerospace Part Accuracy.
Shangqiu JDA Machinery Technology Co., Ltd.
With abundant experience, we are one of the most professional linear milling machine manufacturers and suppliers in China. We warmly welcome you to buy cheap linear milling machine for sale here from our factory. Quality products and reasonable price are available.
Address: No. 55 Pingyuan Middle Road, Liangyuan District, Shangqiu, Henan, China
E-mail: sales@jdamachines.com
WebSite: https://www.jdamachines.com/
