If you’ve ever ordered custom copper turning products—whether for electrical components, architectural accents, plumbing fittings, or medical equipment—you’ve probably wondered: why do some parts fit perfectly, last for years, and look crisp, while others crack, pit, or wear out within months? As a copper turning supplier who’s been in this game for 12 years, I’ve heard that question a hundred times. I’ve also seen too many buyers dismiss quality standards as “manufacturer jargon” until a rush order of faulty valves shut down their entire production line or a custom decorative trim tarnished unevenly 6 months after installation. Today, I want to break down the real, practical quality standards we live by in our shop, no fancy terms, no marketing fluff—just what actually matters when you’re paying for copper turning parts. Copper Turning
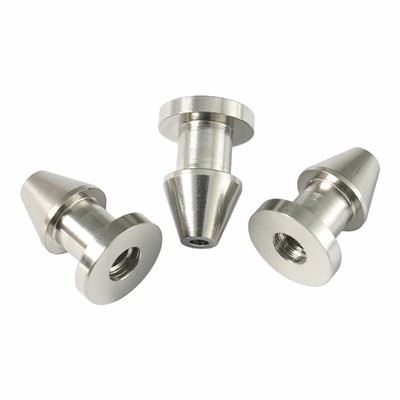
First, let’s start with the foundation: copper alloy selection. This isn’t a trivial choice, and it’s the first line of quality control. A lot of suppliers will grab whatever cheap copper scrap is lying around to cut costs, but that’s a recipe for disaster. For example, C11000 electrolytic tough pitch (ETP) copper is the gold standard for electrical applications because it has 99.90% minimum copper content, which means it has the highest electrical conductivity—critical for busbars, terminals, and connectors. If you use a lower-grade alloy with even a tiny bit of iron or lead mixed in, conductivity drops by 5-10%, which could cause overheating in a power grid component. On the other hand, C36000 free-machining brass (wait, brass is a copper alloy, right) is better for high-volume, complex turning parts like plumbing fittings because it has lead added to make it cut faster without gumming up the lathe. But here’s the catch: C36000 can’t be used for drinking water components in many countries because of lead leaching. We test every batch of copper we receive with a portable X-ray fluorescence (XRF) analyzer to confirm the alloy grade before we even load it into a lathe. No exceptions. If a batch is off-spec, we send it back immediately—even if that means delaying a delivery to a trusted client. I once had a buyer yell at me for a two-day delay when we rejected a 5,000-pound batch of C11000 that had 0.08% iron content instead of the maximum 0.05%. A year later, they told us that delay saved them from a $200,000 product recall because their engineering team would have missed the conductivity issue in pre-production. That’s the kind of small, early check that separates good suppliers from the rest.
Next, the turning process itself—this is where the quality of the part actually gets shaped. A lot of people think turning is just “spinning metal and cutting it with a tool,” but there’s a science to it, and sloppy turning creates defects that are hard to fix later. First, material preparation: before turning, we always anneal copper if it’s going to be formed into complex shapes. Annealing heats the copper to a precise temperature (around 500°C for C11000) to soften it, so it doesn’t crack during turning. If we skip that step, especially for parts with tight tolerances, we get micro-cracks that you can’t see with the naked eye but will open up after a few cycles of pressure or temperature change. Then there’s the lathe setup. We use high-precision CNC lathes with a positioning accuracy of ±0.0005 inches—way tighter than the ±0.005 inches many lower-tier suppliers use. That means when you order a 1-inch diameter pin, it’s going to be exactly 1 inch, not 1.005 or 0.995 inches, so it fits perfectly into your assembly. We also use diamond-tipped cutting tools for the final pass, not carbide tools, which leave a smoother surface finish and reduce the chance of burrs. Burrs are a huge problem—they’re tiny, sharp bits of leftover copper that stick to the edge of a turned part. If you don’t remove them, they can scratch other components, cause leaks, or even cut assembly line workers. We deburr every part manually (for small, complex parts) or with vibratory tumblers (for high-volume simple parts) and then inspect each one under a magnifying glass to make sure no burrs are left. I’ve seen parts that passed dimensional checks have to be scrapped because of a single micro-burr on a critical edge—it’s not worth the risk to our clients.
Surface quality is another big one, and it’s not just about looks. The surface finish of a turned copper part affects everything from corrosion resistance to friction to electrical conductivity. A rough surface has more crevices where moisture and contaminants can get trapped, leading to tarnish or rust (even copper rust, which is actually patina, but it’s uneven and unattractive if it forms on a functional part). For decorative copper trim, a smooth, uniform finish is non-negotiable—clients pay extra for parts that look like they were milled, not cut with a butter knife. We measure surface roughness using a profilometer, which gives us a reading in micro-inches. For electrical connectors, we target a surface roughness of 32 micro-inches or less, because any rougher will reduce contact area and increase resistance. For architectural parts, we go as low as 16 micro-inches for a bright, satin finish. I’ve had clients send us parts from other suppliers that looked shiny but had a roughness of 60 micro-inches—those tarnished in 3 months, while our parts last 5+ years. That’s the kind of long-term quality that matters, not just the initial appearance.
Dimensional tolerance is where a lot of cheap suppliers cut corners, and it’s one of the most frustrating issues for buyers. Let’s say you’re assembling 10,000 copper valves, each requiring a 0.5-inch hole to fit a rubber gasket. If the hole is only 0.49 inches, the gasket won’t fit, and your line stops. If it’s 0.51 inches, the gasket leaks. So what’s an acceptable tolerance? It depends on the part’s function, but for most general turning parts, the standard we follow is ±0.001 inches for critical dimensions, and ±0.002 inches for non-critical dimensions. That’s 10 times tighter than the tolerance many overseas suppliers offer. How do we maintain that? We use coordinate measuring machines (CMMs) to inspect every 10th part in a production run, and for high-precision runs, we inspect every part. We also calibrate all our measuring tools (calipers, micrometers, CMMs) every week—if a micrometer is even slightly off, it can lead to thousands of bad parts. Last year, a client sent us a run of custom copper pins for a medical device, requiring a tolerance of ±0.0008 inches. We inspected the first 100 parts and found a few that were 0.0009 inches off—so we adjusted the lathe’s tool position immediately, before the entire run was done. That saved them from having to scrap 5,000 parts and delay their device launch, which would have cost them hundreds of thousands of dollars in lost revenue.
Corrosion and patina resistance are often overlooked, but copper is a reactive metal—if it’s not treated properly, it will tarnish, and in some cases, corrode. Tarnish is that dull, brownish layer that forms when copper reacts with oxygen and moisture, but for functional parts, especially in outdoor or marine applications, it can lead to failure. We have two ways to address this: first, we can apply a clear, protective coating to the parts—either a lacquer or a powder coat, depending on the application. For medical parts, we use a food-grade, lead-free lacquer that doesn’t leach chemicals. For architectural parts, we can even apply a custom patina that’s uniform and will stop natural tarnishing, so it looks consistent for decades. We also test the corrosion resistance of every batch using a salt spray test—we expose parts to a 5% salt solution at 35°C for 1,000 hours, and if they show more than a 10% tarnish or any pitting, we scrap the entire batch. I once had a client order copper turning parts for a coastal lighthouse project—they thought regular C11000 was enough, but we knew coastal air has high salt content, so we applied a UV-resistant lacquer and did the salt spray test. Two years later, they sent us photos, and the parts looked brand new—while the same parts from another supplier on the same project were already showing heavy tarnish. That’s the difference between following a proper quality standard and cutting corners.
Now, let’s talk about how to actually verify these standards for your own parts, because no supplier is perfect, and you need to make sure they’re delivering what they say. First, ask for material test reports (MTRs) for every batch of copper. A good supplier will have XRF or chemical analysis results that confirm the alloy grade, purity, and any additives. If they can’t provide that, run away. Second, request a sample before placing a large order. Inspect it with a micrometer, a magnifying glass, and if you have access to a profilometer, check the surface roughness. For high-stakes parts, do a small batch test run first, not a full order. Third, ask about their quality control process: do they inspect parts in-process? Do they have a system for tracking defects? What’s their rejection rate? Our rejection rate is less than 0.5%—we only scrap parts that are truly off-spec, and we track every defect to fix our process, not just blame the material.
As a copper turning supplier, our reputation lives or dies by the quality of our parts. We don’t just turn metal—we turn parts that keep power grids running, that seal plumbing systems, that decorate skyscrapers, that save lives in medical devices. That means quality standards aren’t just rules for us—they’re promises to our clients. If you’re looking for copper turning parts that fit perfectly, last, and perform as expected, don’t settle for cheap, off-spec parts that will cause you headaches later. We work with businesses of all sizes, from small startups building new electronics to large construction firms on national projects, and we’re ready to help you find the right copper grade, turning specs, and finish for your application. Whether you need a custom prototype or a 100,000-part production run, we’ve got the processes and standards to deliver quality you can count on. Get in touch with our team to discuss your project, and we’ll be happy to answer any questions you have about our quality control or provide free samples for testing. You won’t regret it.
Aluminum Turned Parts References
ASTM B152/B152M-19, Standard Specification for Copper and Copper Alloy Plate, Sheet, Strip, and Rolled Bar
ISO 11554:2017, Copper and Copper Alloys — Determination of Chemical Composition by X-ray Fluorescence Spectrometry
ASTM E8/E8M-21, Standard Test Methods for Tension Testing of Metallic Materials
NACE TM0172-2016, Method for Laboratory Testing of Metals for Resistance to Sulfide Stress Cracking in Sour Oilfield Environments
Copper Development Association (CDA), “Copper Alloys for Machining and Turning Applications,” 2022
Huizhou Quanyi Precision Hardware Products Co., Ltd.
We’re well-known as one of the leading copper turning manufacturers and suppliers in China, featured by quality products and good service. Please rest assured to buy customized copper turning made in China here from our factory. Contact us for more details.
Address: Building A10, 7th Floor, Zhongchuangyingke 5G Industrial Park, Zhonghan Industrial Park, Tonghu Town, Huizhou City
E-mail: info@qycncturning.com
WebSite: https://www.qycncturning.com/
